CNC Machine Repair: Controls, Spindles, Servos and Electronics

We repair and rebuild CNC controls, spindles, servo drives, and amplifier electronics for FANUC, Haas, Mazak, Okuma, Siemens, and Mitsubishi machines, with on-site and repair-and-return service.

Signs Your CNC Machine Is Failing

A failing CNC machine usually shows warning signs before it goes down completely. Operators notice chatter, unusual spindle noise, burning smells from the electrical cabinet, intermittent axis stalls, or parts drifting out of tolerance. On FANUC-controlled machines, spindle amplifier codes are common indicators: code 01 points to spindle motor overtemperature, code 02 signals a large deviation between commanded and actual spindle speed, code 03 indicates a blown DC-link fuse, code 04 flags an open phase in the incoming power or main circuit, code 06 relates to overspeed or a temperature-sensor fault, and codes 24 and 25 point to communication faults between the CNC and the spindle amplifier.

On Haas controls, alarm 102 (SERVOS OFF), alarms 103-106 (SERVO ERROR TOO LARGE), 108-111 (SERVO OVERLOAD), 135-138 (MOTOR OVERHEAT), and 139-142 (encoder faults) each point toward a specific axis and failure category. Any of these codes, along with rising axis load, vibration, or repeated nuisance trips, is a reason to call for diagnosis before a full failure strands the machine.

Robot Power Supply Repair & PSU Restoration

How CNC Control, Spindle, and Servo Repair Works

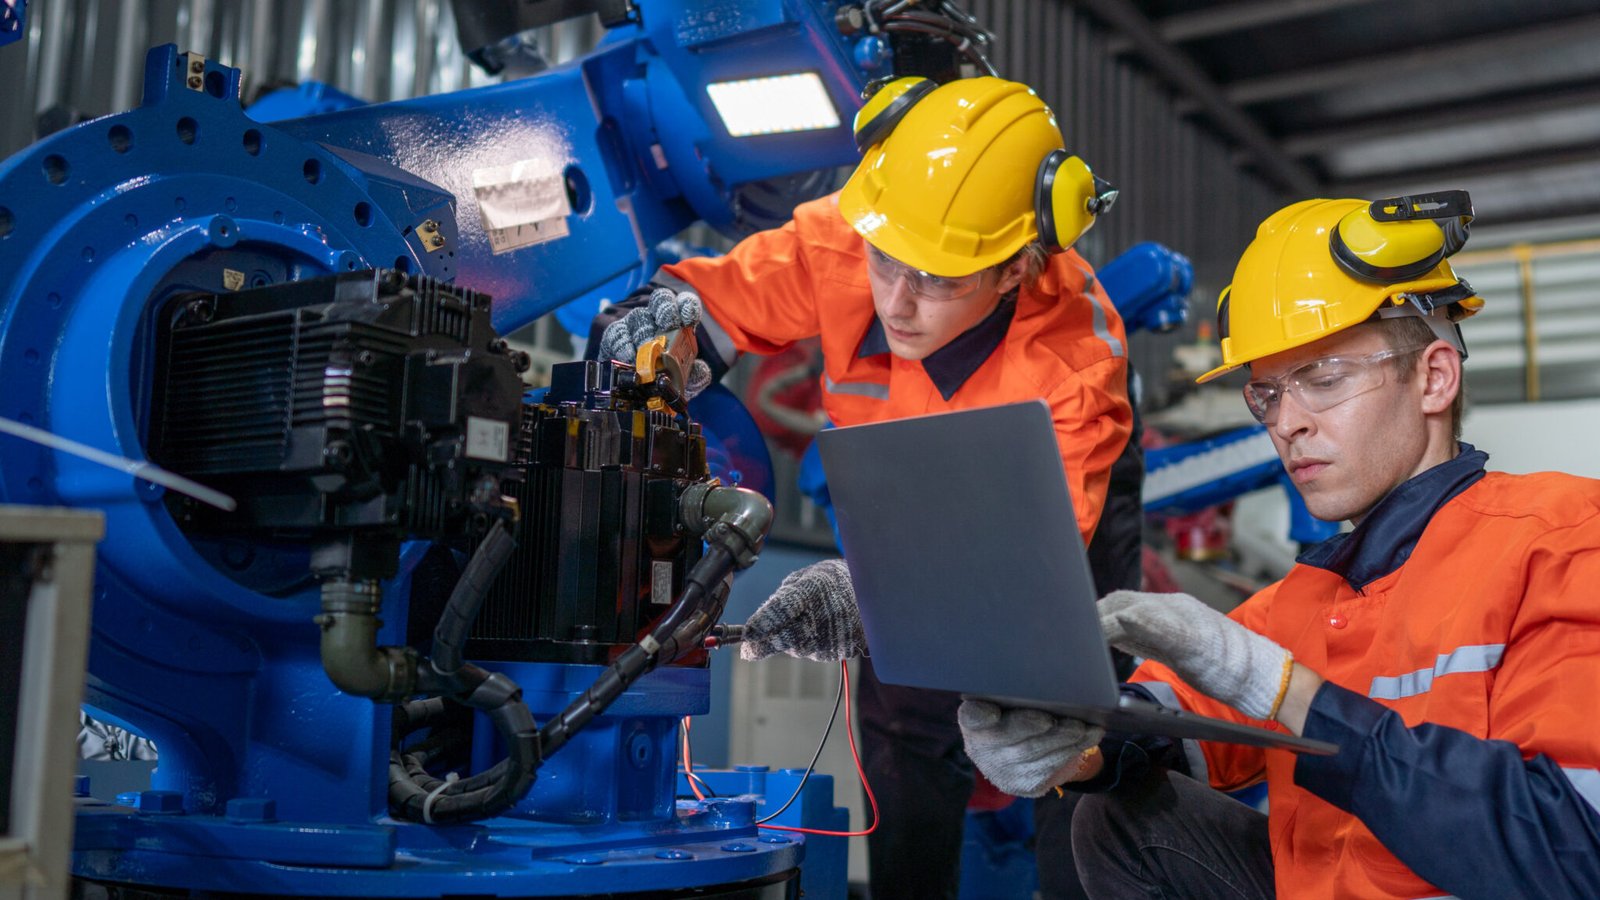
Repair starts with identifying the exact control generation, board assembly number, software or boot version, and machine-builder parameters before any part is replaced or reprogrammed. FANUC amplifier work covers spindle motor modules (SPM), servo motor modules (SVM), and power-supply modules (PSM), including communication faults that occur between them. Component-level work includes visual inspection, cleaning, connector and solder-joint inspection, semiconductor and diode testing, capacitor and resistor testing, relay and contactor checks, and power-supply verification. On Haas amplifiers, DC-bus terminals are checked with a meter using the diode test specified in the model manual, under proper lockout procedures.

Spindle repair covers bearings, encoder or feedback hardware, winding and insulation checks, balancing, seals, cooling components, and taper condition, with the exact scope depending on spindle design and failure evidence. Servo repair addresses the motor, amplifier, encoder feedback, cable carrier, ballscrew, and linear guides, since following-error faults can be electrical or mechanical. We also diagnose cabinets for incoming AC, DC-bus voltage, 24 VDC control voltage, grounding, fan operation, filter condition, and cabinet temperature.

Models and part families we repair include:

  • FANUC alpha and alphai series servo motors, servo amplifiers, and spindle motors, plus SPM, SVM, and PSM amplifier modules
  • Haas servo drives, spindle vector drives, and amplifier assemblies
  • Mazak CNC control and drive assemblies used with Mazatrol systems
  • Okuma OSP control boards and drive units
  • Siemens Sinumerik controls and drive modules
  • Mitsubishi Meldas and Melservo control and servo drive systems

Testing and Verification Before It Ships

Before a repaired control, drive, or spindle ships back, it goes through a controlled power-up sequence confirming the drive reaches ready state without alarms, followed by an alarm-history review, axis homing, and low-speed jogging with feedback verification. Servo repairs are followed by a controlled load test through the axis travel range, comparing current draw against baseline or equivalent axes while watching for following error, vibration, noise, and temperature rise.

Spindle repairs include a no-load speed sweep through the usable RPM range, and a controlled load test on dynamometer equipment when the repair calls for it, recording speed, current, vibration, temperature, and runout. Burn-in testing runs the repaired electronics or spindle for an extended period under controlled conditions to expose intermittent thermal or power-related failures, with duration and limits documented for the specific unit. Final checks cover connector security, insulation and ground-fault results, feedback polarity or phase relationship, cooling airflow, and confirmation that the machine’s stored parameters match what was recorded at intake.

Rebuilding and Replacing Robot Power Supply Units
Benefits of Timely Robot Power Supply Repairs​

Preventing CNC Electrical and Mechanical Failures

Most CNC electronic and mechanical failures give warning before they cause downtime. Cabinet-level maintenance includes cleaning or replacing filters, confirming fan operation, keeping cabinet temperature in range, removing conductive contamination, checking enclosure seals, and keeping coolant out of connectors and electronics. Drag-chain inspection matters because repeated flexing damages motor, encoder, limit-switch, and spindle cables, and an intermittent cable fault can look identical to a drive, motor, or encoder failure.

For servo axes, maintain way lubrication, inspect lube lines, keep way covers clear of chips, check ballscrew and guide condition, and investigate rising axis load before it turns into a following-error alarm. For spindles, maintain the specified cooling system, monitor temperature and vibration trends, use correct lubrication where applicable, check toolholder and taper condition, and avoid sustained operation above the spindle’s rated duty cycle. Trending temperature, current, and vibration over time, rather than waiting for an alarm, catches most failures while they are still a repair instead of a replacement.

Repair vs Replacement for CNC Equipment

A down CNC machine stops production immediately, and the cost of that downtime usually outweighs the repair bill. New replacement units, especially for older FANUC, Haas, Mazak, Okuma, Siemens, and Mitsubishi control and drive generations, can be difficult to source because boards, drives, and motors go obsolete; an exact OEM replacement may require sourcing an equivalent series, transferring parameters, and reviewing software compatibility, which adds lead time on top of the purchase cost.

Repairing the existing control, spindle, or servo system at component level is often faster and less expensive than a full replacement or retrofit, and it avoids the parameter and configuration work that comes with swapping in a different hardware generation. Repair lead time still depends on part availability, failure complexity, and whether the unit is repairable at all, so an exact promise cannot be made without the full part number and diagnostic information. In many cases, though, a repaired spindle or amplifier gets a machine back into production well before a new unit could be sourced and installed.

Why Choose Robotics Integration

Robotics Integration works on FANUC, Haas, Mazak, Okuma, Siemens, and Mitsubishi controls, spindles, servo systems, and cabinet electronics. Because these brands span multiple control and drive generations, the brand name alone is not enough to select a repair procedure or a compatible substitute part; we work from the control model, board assembly number, software version, and machine-builder parameters for each job.

Service is available as repair-and-return for controls, drives, and spindle components, or as on-site diagnosis and repair when the machine cannot be shipped. Quoting starts with intake information for the specific unit: machine make and model, CNC control model, exact alarm text and number, affected axis or spindle, amplifier display code, part numbers and revisions, any recent crash or power event, and the symptoms observed on the machine. That information lets us give a realistic assessment of the failure and the work involved before any repair begins.

Request a CNC Machine Repair Quote

To get a quote on a CNC machine repair, send the machine make and model, the CNC control model, the exact part number and revision on the affected board, drive, motor, or spindle, and the exact alarm text or code displayed. Include a description of when the fault occurs, whether at power-up, under load, during acceleration, or intermittently, and photographs of the nameplate, part labels, and connectors on the affected unit.

This information lets a technician review the failure before committing to a repair path, whether that is component-level electronics repair, spindle rebuild, servo repair, or on-site diagnosis. Call 1-602-449-1556 to discuss a CNC machine repair, a Fanuc CNC repair, a Haas CNC repair, a Mazak service call, or a spindle repair, and to find out what is needed for an accurate quote on the specific unit that is down.

Talk A Robotics Integrator

By submitting this form, you agree to receive communications via phone, text message, and email. Message and data rates may apply. Your information may be shared with trusted third-party service providers solely for the purpose of helping you explore Section Robotic Intergration options. You also agree to our Privacy Policy and Terms of Service.

Success Stories: See What Business Have To Say About Robotics Integration

4.7 Customer Reviews
Business Satisfaction: 98% Delighted with Their Robotics Integration